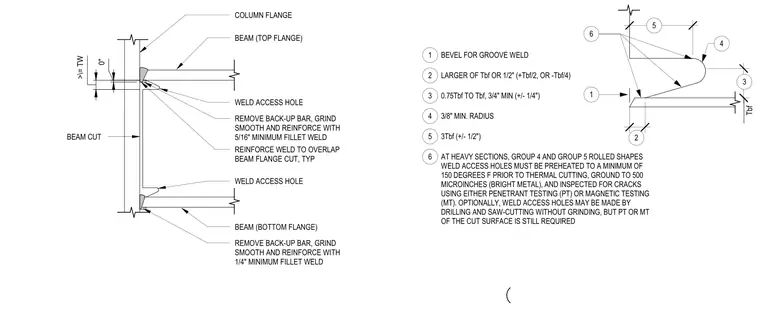
This detail specifies the geometry and finishing requirements for weld access holes at beam-to-column flange connections. The access hole radius is defined as a minimum of 3/8 inch, with the horizontal length set to three times the beam flange thickness plus or minus 1/2 inch. The vertical height is the larger of the beam flange thickness or 1/2 inch, with specific tolerances for the bevel and groove weld preparation. Following the removal of the back-up bar, the area must be ground smooth and reinforced with a 5/16 inch minimum fillet weld at the top flange and a 1/4 inch minimum fillet weld at the bottom flange, ensuring the weld overlaps the beam flange cut. For heavy sections, specifically Group 4 and Group 5 rolled shapes, the access holes require preheating to 150 degrees Fahrenheit prior to thermal cutting, grinding to 500 microinches, and inspection via penetrant or magnetic particle testing.
Members view this detail in full resolution, download the CAD files (SVG, PDF), and can adapt it in the built-in CAD editor — export DXF, DWG, or PDF.
Start membership